Efficient Metal Shops and Slow Ones Are Often Separated by Ironworker Tooling
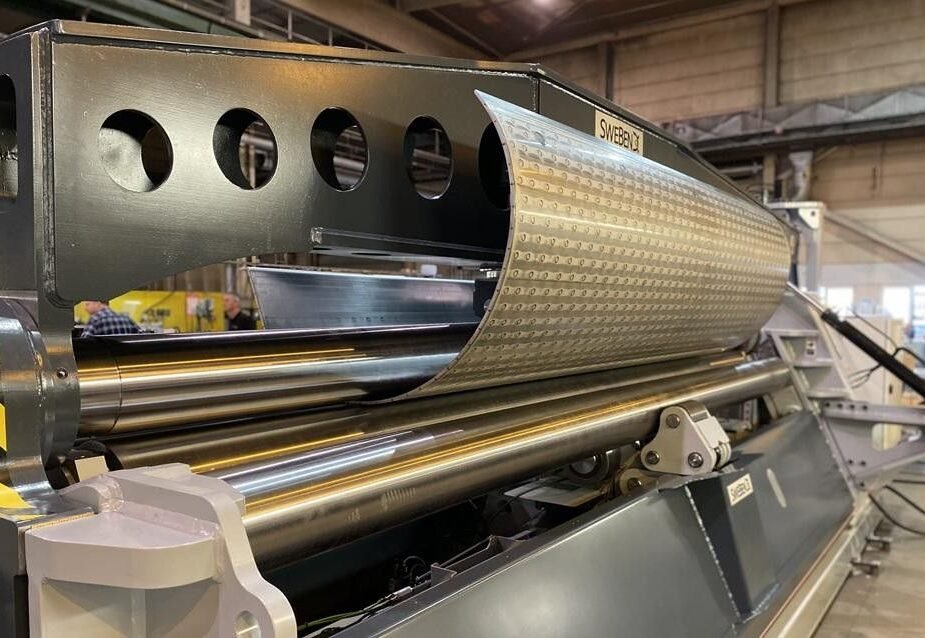
An ironworker’s capacity depends on more than hydraulic force. The punch, die, shear, brake, and accessory installed on the machine determine how efficiently a shop cuts, forms, and prepares metal.
Suitable tooling reduces setup changes, improves repeatability, and gives operators more ways to complete work without moving material between machines.
The right selection also supports safer operation because each tool matches a defined task, material, and machine capacity. Several tooling choices deserve close attention.
Match Tooling to the Work
A shop should begin with its recurring jobs rather than selecting accessories by appearance. Punching holes, trimming corners, bending flat stock, notching pipe, and shearing Unistrut each require a different tool. Matching the accessory to the work reduces improvised setups and keeps the operator’s process consistent.
For shops reviewing options, essential tools for ironworkers and metal fabrication include punches and dies, brakes, notchers, shears, and specialty accessories. These tools connect directly to compatible ironworkers and expand the machine’s work range. The selection should reflect the material sizes, shapes, and production tasks that appear most often in the shop.
Start With Punches and Dies
Punches and dies affect hole quality, alignment, and setup time. Scotchman provides round, round offset, metric, oval, square, corner-turning, hexagon, picket, trimming, and cut-off shapes for its ironworkers. Shaped punches use standard keying for positive alignment during operation.
Operators must pair the punch and die correctly. Proper alignment protects the tooling and supports safe punching. Material thickness also matters. The manufacturer’s guidance states that operators should never punch material thicker than the punch diameter.
A shop should label stored sets by size, shape, and machine model. That small control prevents mismatched components from reaching the tool station and shortens selection time during production.
Add Forming Capacity With Brakes
An ironworker brake handles forming work that would otherwise require a separate press brake or manual process. The 8-inch brake delivers 25 tons of force and bends metal up to 8 inches wide with a 2-inch lower V-die. It is available for the Porta Fab 45, 50514-EC, and 5014-ET models.
A brake table with a scale and squaring arm improves positioning for repeated bends. The operator can set the material against a consistent reference point, reducing measurement variation between parts. This matters when several pieces must match during assembly.
Use Notchers for Clean Pipe Joints
A pipe notcher creates a gap-free notch in seconds when the correct die set matches the pipe. The accessory works in the tool table or punch station on most models and requires Schedule 40 pipe notcher die sets.
Available standard sizes include 3/4 inch, 1 inch, 1-1/4 inches, 1-1/2 inches, and 2 inches. Selecting the die before production prevents poor-fitting joints and eliminates repeated hand fitting. The operator should confirm pipe size and wall requirements before installing the tooling.
Choose Specialty Tools for Repeat Jobs
Specialty accessories become useful when a shop performs the same preparation task regularly. A picket tool flattens and trims 1/2-inch, 3/4-inch, or 1-inch thin-gauge hollow-wall square tubing. Separate dies are required for each size.
A Unistrut shear cuts Unistrut without distortion, which helps preserve the channel’s usable profile. A weld coupon bender bends welded coupons so an instructor or student can identify weak points in a weld. These tools keep focused tasks at the ironworker instead of sending material to another station.
The LED work light for the Porta-Fab 45 punch station improves visibility around the work area. It is a factory-installed option, so it must be considered when ordering the machine rather than added later.
Control Setup, Storage, and Maintenance
Tooling efficiency depends on access and condition as much as tool selection. A punch and die storage drawer keeps commonly used sets together and reduces time spent searching through loose components. A snap ring removal tool also simplifies maintenance for style #20 punches.
Operators should inspect punch edges, die openings, retaining components, and alignment before use. Worn or damaged tooling affects cut quality and places extra strain on the machine. Storage records should identify compatible models, sizes, and replacement requirements.
Training matters as well. Operators need clear instructions for standard and offset dies, correct installation, and safe material limits. A short setup check prevents errors that can damage tooling or stop production.
Conclusion
Efficient metal shops treat ironworker tooling as part of production planning, not as an accessory purchased after the machine arrives. The best starting point is a list of recurring operations, material sizes, and machine models. That list can guide punch and die selection, brake capacity, pipe notcher sizing, and specialty tool choices.
Before the next order, review the shop’s most repeated jobs and match each one with a compatible accessory, storage method, and operator procedure.
Last modified: October 8, 2026